Most shops keep running a cold saw blade until the parts fail inspection, and by then the blade has already cost more in scrap and spindle load than a sharpening would have. The decision between sharpening, retipping and replacing is not a judgement call once you know which signals to read. This guide gives you six indicators you can check in a two-minute walk-around, a simple record that turns blade decisions into arithmetic, and the point at which no maintenance will save the blade.
Check these in order. The first four you can see or hear without instruments; the last two need a stopwatch and a micrometer.
Measure the burr on three pieces from the same bar and compare with the reading you took when the blade was new. A sharp blade produces a small, even burr. A worn blade produces a taller, irregular burr with a rolled-over edge that catches a fingernail. Doubling is the practical trigger, not a fixed number, because acceptable burr depends on your next operation.
A cutting edge leaves fine machining marks. A worn edge rubs, and rubbing polishes. If the cut face looks bright and mirror-like where it used to look matte, the tooth is no longer shearing the metal, it is burnishing it. That also means the blade is generating heat and work-hardening the cut zone, which makes the next cut harder still.
Operators hear this before anyone measures it. A dull blade on a cold saw produces a higher, harsher note and a rhythmic thump as worn teeth pass through the cut. If the machine sounds different on Monday than it did on Friday with the same material, check the blade before you check the spindle.
Watch the load meter through a normal cut. A dull blade needs more force for the same chip, so load creeps upward, and on a machine with a load limit the cycle starts to slow or stall. A 10 to 15 percent rise over the baseline is a reliable early warning, well before part quality drops.
Time a single cut with a stopwatch when the blade is new, then check it weekly. A 20 percent increase in cycle time on the same material and section is wear you can see in the numbers. On a high-volume line this is also the easiest cost to put in front of management, because it converts directly into lost pieces per shift.
A dull blade deflects rather than cuts, and deflection shows up as an out-of-square end or a slight taper across the wall. Check with a square and feeler gauge on a thick-wall piece. If squareness drifts on the same machine setting that used to hold, and the clamp and guides are sound, the blade is the remaining variable.
| Signal | Meaning | Action |
|---|---|---|
| Burr up, sound normal | Edge wear starting | Sharpen at next planned stop |
| Burr up, load up, sound harsh | Edge worn through | Sharpen now, do not finish the shift |
| Chipped or missing teeth | Impact damage, wrong feed, material flaw | Sharpen if the chip is small, replace if teeth are lost |
| Cracks from the gullet | Fatigue, usually from vibration or wrong tension | Replace, and check the machine before fitting a new one |
| Blade below minimum diameter | Too many grinds | Replace, the geometry no longer matches the machine |
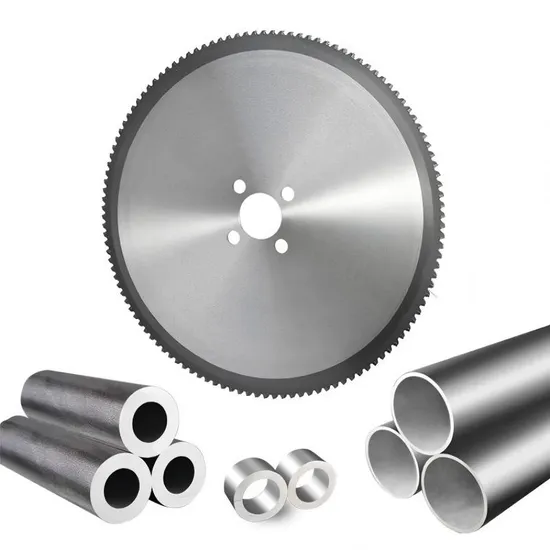
The answer depends on what kind of blade you are holding. A solid HSS cold saw blade is ground back and reused several times. A carbide-tipped blade can be ground back while the tips are intact, and retipped once or twice when they are not. A blade with cracks in the plate, a bent body or a worn bore cannot be saved by either process.
| Condition | Best route | Why |
|---|---|---|
| Uniform wear, teeth intact | Sharpen | Cheapest per cut, restores geometry |
| Chipped tips, body sound | Sharpen if minor, retip if widespread | Retipping costs more but returns full tooth height |
| Cracks, bends, worn bore | Replace | The plate is the structure; a cracked plate is scrap |
| Below minimum diameter after grinding | Replace | Blade speed and clearance no longer match the saw |
Every grind removes material from the tooth face and reduces the outside diameter slightly. That is why a blade has a finite number of lives, and why you should write the current diameter on the blade after each service. Once it drops below the machine’s minimum, the surface speed at the tooth is wrong and no amount of sharpening will bring the cut back.
Burning through blades faster than you should?
A blade that fails early usually points at feed, coolant or blade choice. Tell us the material, the section, the blade you run and the pieces per blade you get, and we will tell you whether the fix is a different blade or a different setting.
Put a card next to the machine and write four numbers on it every shift: pieces cut since the blade was fitted, burr height, cycle time for one cut, and load reading at mid-cut. That is all. Within two weeks you will see the trend before the parts go bad, and the sharpening decision becomes a date on a calendar rather than a panic at the inspection bench.
Keep the same record across blades and you also get the number that matters commercially: pieces per blade. That single figure lets you compare a cheap blade against an expensive one honestly, and it usually shows that the cheap blade costs more per cut than it saved at the counter.
How much does sharpening remove from a blade?
Typically a few tenths of a millimetre from the tooth face per service, more if the teeth are chipped. That is why the diameter has to be recorded each time; three or four services can take a blade from comfortable to below the machine minimum.
Can I sharpen a blade in house?
Only with a proper tooth grinding machine and the right wheel for the tooth geometry. Hand grinding or a general-purpose grinder changes the rake angle and the blade will never cut the same. For most shops, sending blades out is cheaper than doing it badly.
Why did a freshly sharpened blade cut worse than before?
Three likely reasons: the tooth set was not restored, the rake angle was changed by the grind, or the blade was refitted with a burr on the bore. Check the set first; a blade with insufficient set rubs on the side and overheats.
Is it worth retipping a blade rather than buying new?
Usually yes if the plate is sound, because retipping restores full tooth height and gives you a blade that behaves like new. It stops being worthwhile when the plate has been ground thin or the body is distorted, so ask for an inspection before authorising the work.
What causes teeth to chip on the entry side?
Usually a feed that is too aggressive on entry, or material that is not flat against the table so the blade meets an edge rather than a face. Reduce the entry feed and check that the tube is fully seated before the head descends.
Does coolant quality affect how often I sharpen?
Directly. A weak or dirty mix raises friction and temperature, and the edge dulls faster. Keep the concentration at the maker’s figure, skim tramp oil and change the tank on schedule; it is the cheapest way to extend the interval between grinds.
How should a blade be stored between services?
Flat or in a proper rack, protected from the teeth touching anything hard, and never hung on a nail. A blade stored on a hook develops a bend that shows up as runout and uneven cut for the rest of its life.
Can I use a blade after it has cut aluminum to cut steel?
No. Aluminum embeds in the tooth edge and changes the geometry, and the edges that suit aluminum are too sharp for steel. Keep separate blades per material family and label them clearly.
How do I check the blade for cracks?
Clean it, hold it against a light and inspect the gullet roots with a magnifier, especially on high-tooth-count blades. Cracks start at the gullet and run outward, and they are the one defect you must never sharpen past.
Is a blade change worth scheduling every shift?
No, but checking the blade every shift is. A two-minute inspection catches the chipped tooth before the cascade, and a spare blade on the shelf means the change happens at a planned stop rather than in the middle of a hot order.
Keep reading
Understand the cutting method in circular cold saws vs conventional saws, and the common errors in mistakes to avoid when choosing saw blades.
Equipment
See the flying cut cold saw blade for tube, the TCT saw blade range and the circular cold saw category.
Sharpen at the first sign of rising burr and load, retip while the plate is sound, and replace only when the blade is out of geometry or cracked. The four numbers on the card next to the machine will tell you which of those you are looking at, and they will show you the moment a poor blade choice is costing more than a good one would. Track pieces per blade for a month and the decision stops being an argument.
Contact us if you have any questions we will reply as soon aspossible